Owner-Side Project Manager · PMP

Alexander SantanaPMP

Alex runs technical, heavily regulated facility projects from the owner’s side. He has done the hard version: invented the process, built and commissioned the plants, and got a hazardous facility certified and occupied.

Atlantic Beach, FL · Northeast Florida

Simplified flow diagram of the Riviera Beach plants Natural gas enters a plasma reactor powered by a microwave generator. Hydrogen leaves on one line. Acetylene leaves on another and passes through temperature swing adsorber purification. NATURAL GAS MICROWAVE GENERATOR PLASMA REACTOR HYDROGEN TSA PURIFICATION ACETYLENE
What the Riviera Beach plants do: natural gas in, hydrogen and acetylene out. Simplified.

Inside the pilot plant

Riviera Beach, FL · 360° walkthrough · 1:24
Pilot plant 360° walkthrough · 1:24

A slow pan through the ~$6M pilot plant: a facility housing explosive, flammable gases and high-voltage equipment above 20 kV, certified and occupied.

Read the project →

Selected projects

7 sheets · 2020–2026

Riviera Beach demonstration and pilot plants
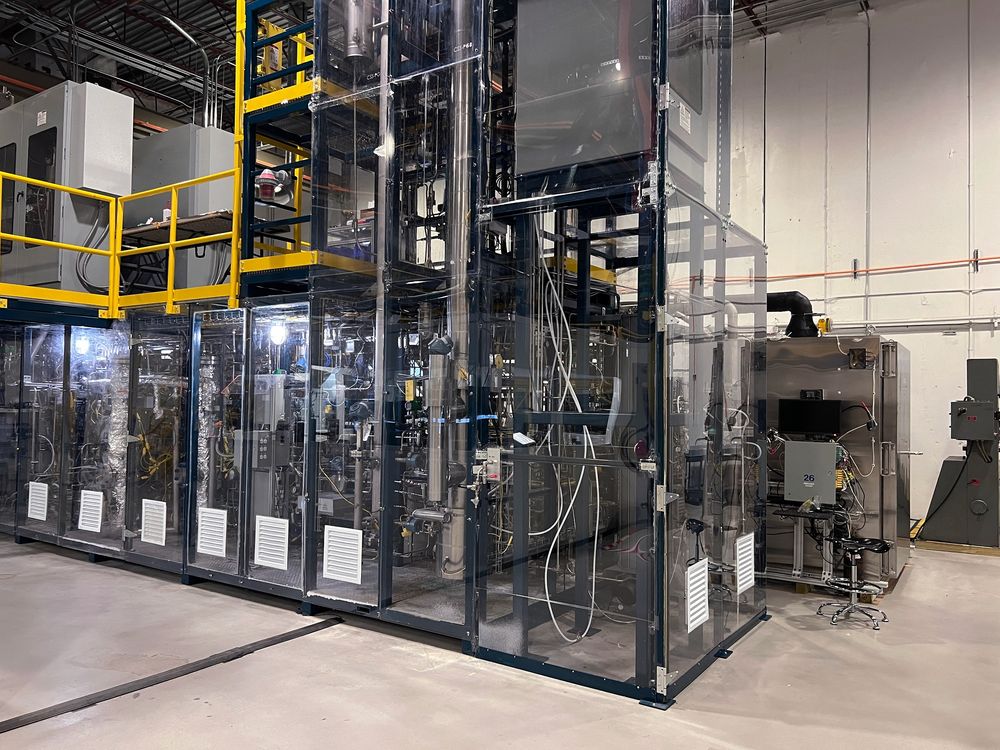
The pilot plant inside its building: process equipment in glass-walled enclosures, with yellow-railed platforms above.
Pilot plant, Riviera Beach
SHEET 01 / 07
Scale
$2M + $6Mtwo plants, built and commissioned
Place
Riviera Beach, FL
Years
2020–2022
Role
Senior Project Engineer; project lead, design through startup

Two microwave-plasma plants that turn natural gas into hydrogen and acetylene. Both were delivered on budget and on schedule, in a building certified to hold explosive gases and high-voltage equipment.

Full story and key facts
Challenge
A new process had to become a working, permitted facility. The building would house explosive, flammable gases next to novel high-voltage equipment running above 20 kV (20,000 volts).
What he did

Took both plants through every stage: permitting, front-end engineering design (FEED, the early design that fixes scope and cost), process-safety reviews (HAZOP), detailed design, fabrication, factory acceptance testing (proving equipment at the maker’s shop before it ships), construction, commissioning and operations.

The ~$2M demonstration plant was designed and built in-house. The ~$6M pilot plant was executed with engineering-procurement-construction (EPC) contractors.

Result
Secured UL certification and a certificate of occupancy. Both plants were delivered on budget and on schedule. The demonstration plant finished ahead of schedule and ran successfully on its first startup, with more than 99% uptime at full product purity.
  • ~$2M demonstration plant, designed and built in-house
  • ~$6M pilot plant, executed with EPC contractors
  • UL certification and certificate of occupancy
  • >20 kV high-voltage equipment
  • >99% uptime at full product purity
  • Successful first startup, ahead of schedule
Watch the 360° walkthrough ↑

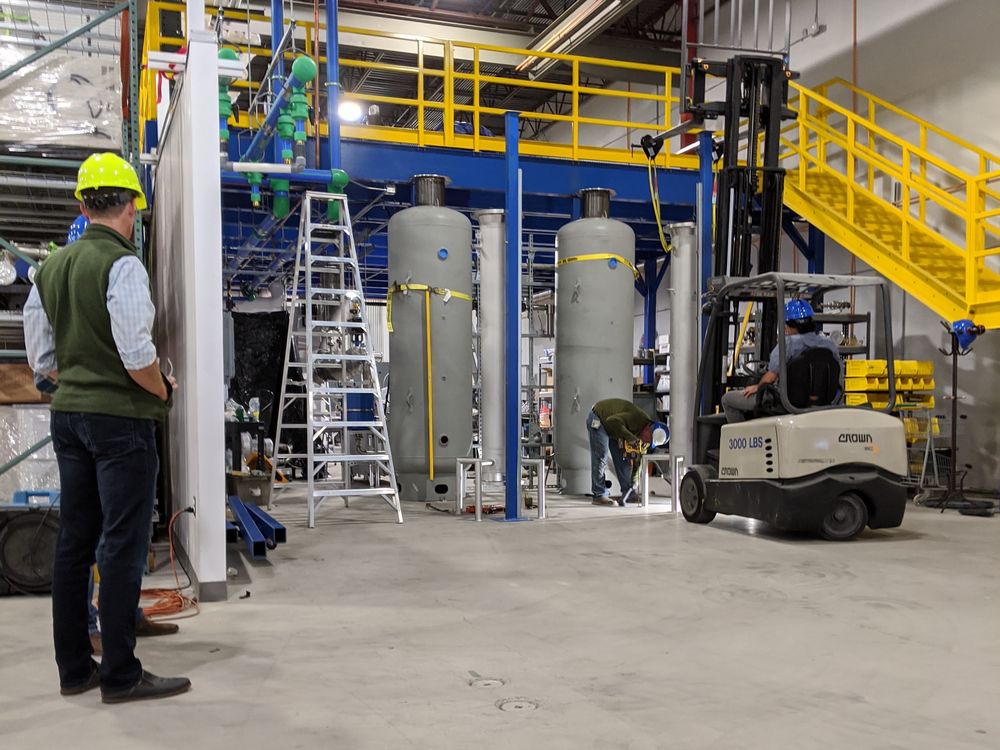
Acetylene purification units (TSA)

Tall purification vessels being installed in the plant building, with a forklift, a ladder and a technician at work.
TSA units during installation
SHEET 02 / 07
Scale
US 11,285,427lead inventor on the purification method these units use
Place
Riviera Beach, FL
Years
2020–2021
Role
Design-build lead and inventor

Commercial-scale units that purify explosive acetylene for the demonstration plant. Alex invented the approach, led the build, did much of the trade work himself, and the units ran on the first attempt.

Full story and key facts
Challenge
The demonstration plant needed its acetylene purified at commercial scale, and acetylene is explosive. A temperature swing adsorber (TSA) cleans a gas by trapping impurities on a solid, then heating the solid to release them and start again. No commercial unit existed for this gas stream, and a small team had to invent, build and start the units on the plant’s schedule.
What he did
Led the design-build of multiple TSA units and directed the team through in-house design, execution and operation. Personally did the plumbing, electrical, structural, instrumentation and controls work, and erected the units with forklift, scissor and articulating lifts. Led commissioning and troubleshooting.
Result
The units operated successfully on the first attempt. The purification approach is patented: Alex is lead inventor on US 11,285,427, “Systems and methods for acetylene purification”.
  • Multiple commercial-scale TSA units
  • Designed, built and operated in-house
  • Hands-on: plumbing, electrical, structural, instrumentation, controls
  • Operated successfully on the first attempt

Kentucky plant turnaround

SHEET 03 / 07
Scale
$85M → $45Mcapital cost after a ground-up redesign · 1,800 TPY (tons per year)
Place
Calvert City, KY
Years
2022–2024
Role
Lead owner’s-representative engineer

The first estimate for a commercial acetylene plant came in near $85M. Alex led a ground-up redesign that brought the capital cost to $45M, and the client signed a contract to build.

Full story and key facts
Challenge
Front-end engineering design (FEED) for a commercial plant producing 1,800 tons per year of acetylene for a national industrial gas client. The first capital estimate came in at about $85M. The EPC partner was drifting off scope and schedule, and at that price the plant no longer made economic sense for the client.
What he did

Led a ground-up redesign that challenged every design assumption: a novel reactor design, absorption column sizing, process simulations, heat exchanger sizing, bulk hydrogen compression and storage, bulk acetylene storage, and the plant control narrative.

Managed the engineering-procurement-construction (EPC) partner in Houston, with regular travel, and put a corrective action plan in place to keep the partner on scope and schedule.

Result
Capital cost came down from about $85M to $45M, and the client signed a contract to build. The project ended when the company closed.
  • 1,800 TPY commercial acetylene facility
  • ~$85M first estimate; $45M after redesign
  • EPC partner in Houston, managed on site and remotely
  • Corrective action plan for scope and schedule
  • Client signed a contract to build

Japan plant for Denka

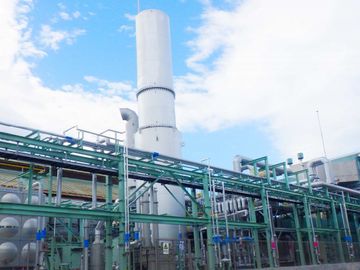
A Denka chemical plant: a tall white column beside green pipe racks.
Denka plant · Photo: Denka
SHEET 04 / 07
Scale
~1,600 TPYacetylene facility, design adapted for Japan
Place
Omuta, Japan
Years
2023–2024
Role
Lead owner’s-representative engineer

Adapted a U.S. plant design for a Japanese site: a different feed gas, different impurities, the customer’s specifications and Japanese regulations, working across language and time zones.

Full story and key facts
Challenge
Denka and Transform Materials signed a multi-year facility development and installation agreement in May 2023. The design had to be localized for Japan, which meant changing the feed gas from natural gas to propane and meeting Japanese regulations.
What he did
Led the front-end engineering design (FEED) localization. Adapted the design for the new feed gas, its impurity profile, the customer’s specifications and Japanese regulations. Worked across cultural, language and time-zone barriers, and found a Japanese engineering-procurement-construction (EPC) partner.
Result
The work won a signed contract to proceed to detailed design and construction. The company’s closure ended the project before construction.
  • ~1,600 TPY acetylene facility
  • Feed gas changed from natural gas to propane
  • Designed to Japanese regulations
  • Japanese EPC partner found and engaged

~$2B plant feasibility and redesign

SHEET 05 / 07
Scale
~$2Bplant designed and estimated for the client’s review
Client
A major Indian industrial conglomerate
Years
2023–2024
Role
Lead process engineer, technology licensor

Designed and estimated a roughly $2B plant that a major Indian industrial conglomerate was to build under license from Transform Materials. The technology had to be fundamentally redesigned to work at that size.

Full story and key facts
Challenge
As the technology licensor (the company that owns the process and licenses it to the plant owner), Transform had to deliver a design the client’s own engineering team would review in detail, at a scale far beyond anything built before.
What he did
Fundamentally redesigned the technology for that scale. Worked with the industry’s leading microwave equipment manufacturers and pushed them to build generators at a size not built before. Produced the feasibility study, cost estimate and engineering documents for the client’s approval.
Result
The client’s engineering team reviewed the package and approved moving to the next phase. The company’s closure ended the project.
  • ~$2B plant design and cost estimate
  • Technology redesigned for scale
  • Generator makers pushed to a new size
  • Feasibility study and engineering documents delivered for client review
  • Client approved the next phase

Microwave generator procurement

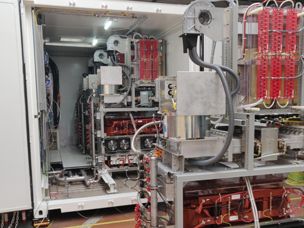
Microwave generator equipment and red power modules inside an open shipping container.
Microwave generator equipment
SHEET 06 / 07
Scale
$4.5Minternational equipment purchase
Place
Factory testing in Lyon, France
Years
2022–2024
Role
Owner’s-representative engineer, procurement lead

Ran a $4.5M international purchase of microwave generators for the Japan plant, from the first request for quotation to in-person factory acceptance testing at SAIREM in Lyon.

Full story and key facts
Challenge
The generators had to fit a smaller footprint than usual. At factory acceptance testing (proving equipment at the maker’s shop before it ships), the equipment missed its required power specification.
What he did
Ran the international bid from request for quotation to in-person testing. Re-engineered the equipment with vendors to fit the smaller footprint. When the equipment missed its power specification, worked hands-on with SAIREM on the fix and pushed it through to completion.
Result
The generators passed a second round of factory acceptance testing, at power levels that pushed the limits of the industry. They were held in France until construction of the Japan plant was to start.
  • $4.5M purchase
  • Vendor: SAIREM
  • In-person factory acceptance testing, Lyon
  • Smaller footprint than usual
  • Passed a second round of acceptance testing

Production scale-up for MFG Merch

SHEET 07 / 07
Scale
130%year-over-year sales growth the expanded operation supported
Place
Jacksonville, FL
Years
2025–2026
Role
Process Engineering Consultant

Scaled production for the exclusive merchandise manufacturer for Unrivaled, the women’s professional basketball league, then handed a working operation to a permanent manager.

Full story and key facts
Challenge
Demand was outgrowing a largely manual operation with no inventory system or written procedures.
What he did
Scaled production capacity. Implemented barcode-verified warehouse management. Built and trained the team, wrote the standard operating procedures, and hired the permanent manager before handing off.
Result
The expanded operation supported 130% year-over-year sales growth.
  • 130% year-over-year sales growth supported
  • Barcode-verified warehouse management
  • Team built and trained; procedures written
  • Permanent manager hired before handoff

Patents

7 issued in the U.S. · inventor
  1. US 11,285,427 B2Systems and methods for acetylene purification2022Lead inventor
  2. US 10,676,353 B2Systems and methods for processing gases2020Co-inventor
  3. US 11,471,852 B2Systems and methods for processing gases2022Co-inventor
  4. US 11,633,710 B2Systems and methods for processing gases2023Co-inventor
  5. US 11,634,323 B2Systems and methods for processing gases2023Co-inventor
  6. US 11,634,324 B2Systems and methods for processing gases2023Co-inventor
  7. US 12,215,026 B2Systems and methods for processing gases2025Co-inventor

Granted counterparts in Japan (JP 7705592 B2, JP 7808646 B2), Australia (AU 2019325589 B2) and China (CN 112867702 B).

Experience

2016–present
Alex presenting to a crowd of visitors at the Transform Materials booth at a conference.
Presenting Transform Materials’ technology at an industry conference in Houston.
  1. 2026–present
    Owner-side project management consultingCommercial construction of an aquatic facility
  2. 2025–2026
    Process Engineering ConsultantMFG Merch · Jacksonville, FL
  3. 2022–2024
    Senior Process EngineerTransform Materials · Riviera Beach, FL
  4. 2021–2022
    Senior Project EngineerTransform Materials · Riviera Beach, FL
  5. 2016–2021
    Senior Research ScientistTransform Materials · Riviera Beach, FL
  6. 2016
    B.S. ChemistryFlorida Atlantic University

Transform Materials developed microwave-plasma conversion of natural gas to hydrogen and acetylene. The company has since closed; its technology and patents were sold.

Chart Industries took a 5% equity stake for $25M and signed a binding commercial memorandum of understanding in March 2021. Partners included Denka, DSM (technology license, 2020) and Johnson Matthey (collaboration, 2024).

  • PMP

Community

2005–present
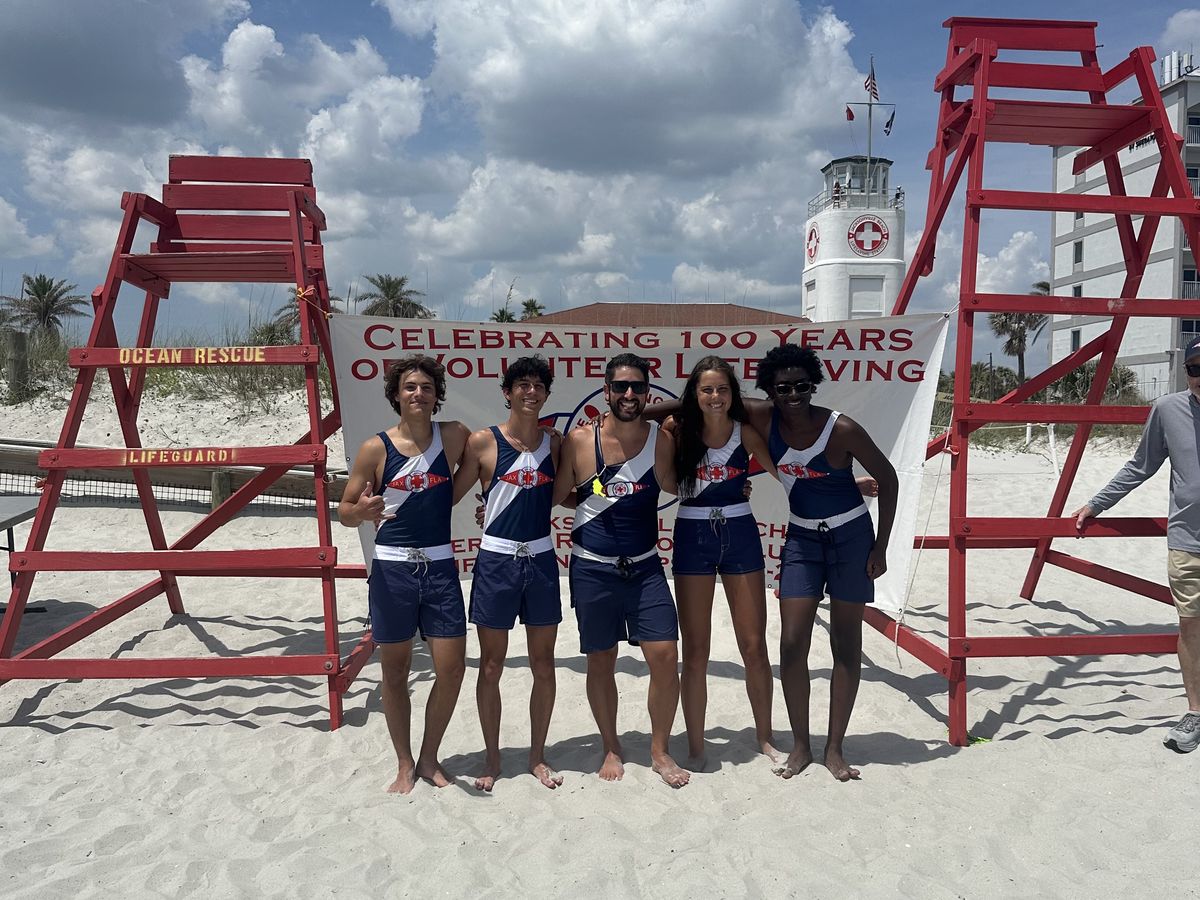
Five Corps lifeguards in uniform on the beach between two red lifeguard stands, under a banner celebrating 100 years of volunteer lifesaving.
Corps lifeguards at Jacksonville Beach.

Volunteer Life Saving Corps (VLSC), Jacksonville Beach: a corps of volunteer ocean lifeguards. Alex joined in 2005, when it was the American Red Cross Volunteer Life Saving Corps.

  • 1,000+ volunteer hours
  • Elected to staff leadership
  • Rescue swimmer
  • Multiple American Red Cross Lifesaving Awards
  • EMT-B · CPR Instructor · Rescue Diver

Contact

Based in Atlantic Beach and looking for a long-term project management role in Northeast Florida.

Email
alex@AlexSantanaPMP.com
LinkedIn
linkedin.com/in/alexander-o-santana

References available on request.